
Automotive wire harness assembly
Wire Harness Assembly for Automotive Programs
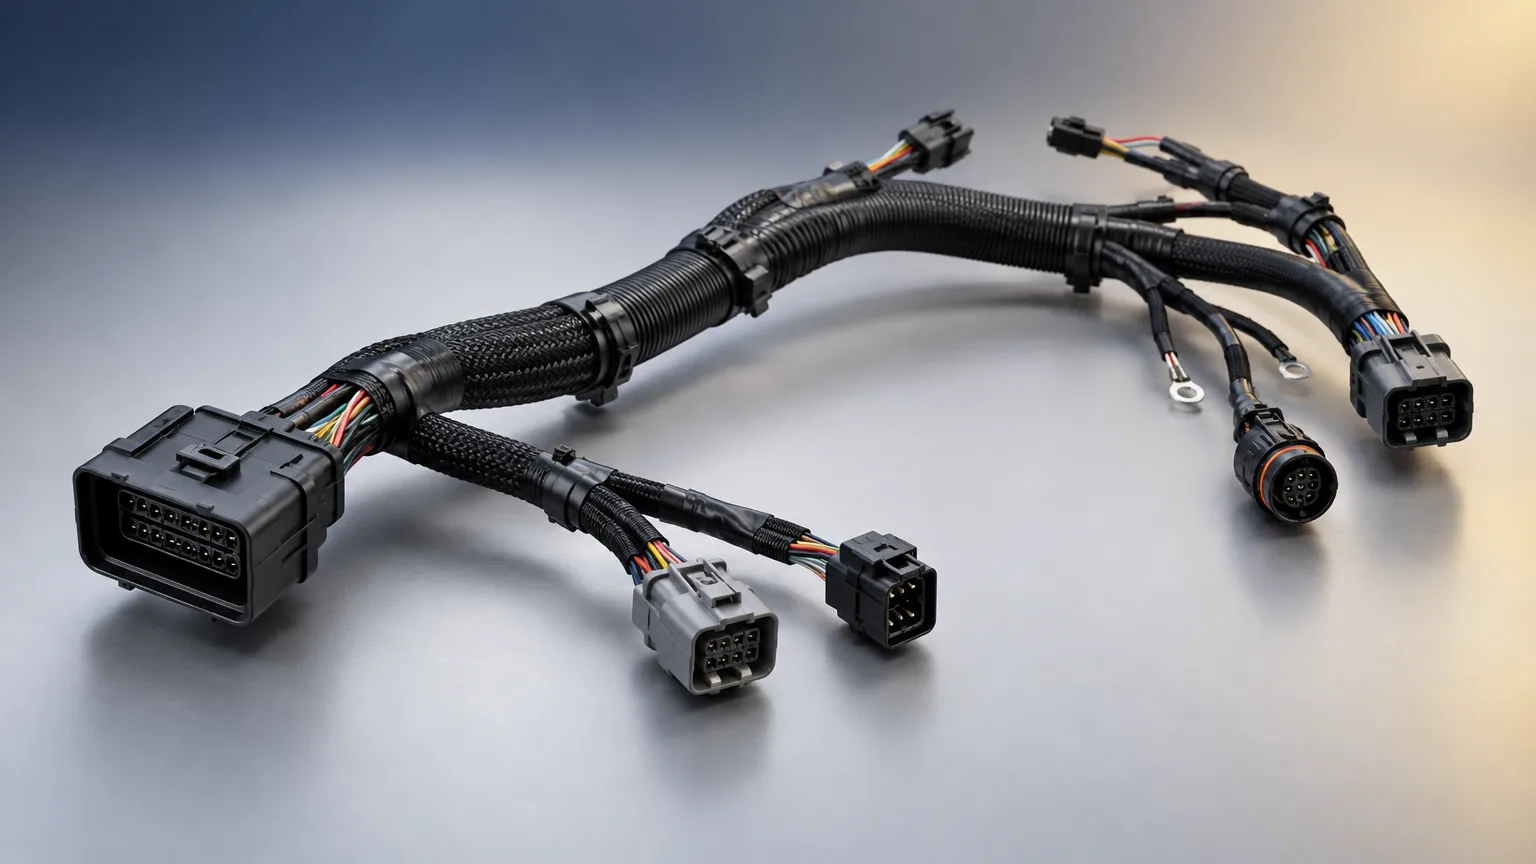
Wire harness assembly is the cutting, crimping, sealing, routing and testing of cable assemblies built to a drawing. SR collects quotes from a vetted supplier network, manages quality and inspection, and delivers parts.
- Cable harness assembly
- Cut, crimp, seal, test
- Drawing-based builds
- Inspection managed by SR
- Vetted supplier networkQuotes collected from approved harness builders
- Inspection managedContinuity, pull and dimensional checks
- Quote turnaroundWorking days from complete RFQ package
Wire harness assembly is the process of cutting cable to length, stripping and crimping terminals, inserting seals and connectors, bundling the runs, and testing continuity and pull strength to a released drawing. Automotive wire harness work suits prototype builds through production programs where routing, connector families and test evidence must match the customer's requirements.
What wire harness assembly is and when to use it
Wire harness assembly is the production of a cable harness assembly to a released drawing: cable is cut to length, terminals are crimped, seals and connectors are fitted, branches are bundled, and the finished harness is tested. It is a build-to-print service, not a catalog item, so the drawing and bill of materials define the part.
The service fits engineers and procurement teams who need automotive wire harnesses for a vehicle program, a test fleet, or a service part. It is the right route when connector families, wire gauges, branch lengths and test evidence must be controlled and repeatable across builds.
When to use a harness assembly supplier
- You have a drawing, a wire list or a sample harness that can be documented.
- The build needs crimped terminals, sealed connectors or overmolded joints rather than loose cable.
- Continuity, pull strength or dimensional checks must be recorded for each unit.
- Volume is moving from a bench prototype to a repeatable batch or production program.
- The program falls under IATF 16949 and customer-specific requirements, so process control and traceability matter.
Wire harness assembly process steps
Wire harness assembly is the process of cutting, terminating, routing and testing cables into one bundle that connects vehicle electrical components. In automotive parts manufacturing, the harness is built to a drawing, wire list and connector schedule, then tested before delivery.
The same sequence applies in auto parts manufacturing, car parts manufacturing and vehicle parts manufacturing programs. Automotive component manufacturers agree the drawing package and test plan before cutting starts.
- 1. Drawing and BOM review The supplier reviews the drawing, wire list, connector schedule and bill of materials. Missing gauges, terminal part numbers or branch lengths are flagged before quoting.
- 2. Material and component verification Incoming cable, terminals, seals, connectors and sleeving are checked against the specification, with certification review where required. Traceability starts here.
- 3. Cutting and stripping Cable is cut to the wire-list lengths and stripped to the length the terminal requires, typically about 0.2 in (5 mm). Strip length and cut length most often drive rework.
- 4. Crimping and seal insertion Terminals are crimped to the conductor and insulation, and seals are inserted where the connector family calls for them. Crimp height, pull strength and visual criteria follow the drawing and control plan.
- 5. Connector loading and routing Leads are loaded into the cavity positions shown on the drawing, then routed and bundled into branches. Branch lengths, breakouts and tie positions follow the drawing.
- 6. Joining and protection Splices, welds, bonding or overmolding are added where specified, and the bundle is protected with tape, conduit, sleeving or boots. Joint strength, distortion and traceability require validation.
- 7. Electrical and dimensional test Continuity, short and miswire checks run against the wire list, with pull tests and dimensional checks on critical features. Results are recorded for the build.
- 8. Inspection, packing and delivery Final inspection confirms the harness matches the approved drawing and test record. Parts are packed to protect connectors and branches, then shipped to the purchase-order location.
Materials and finishes for automotive wire harnesses
Automotive components such as harnesses use material families set by the drawing and the vehicle environment. The table lists families that appear in harness work; grades are not verified here and must be specified by the drawing.
| Material | Properties | Typical uses |
|---|---|---|
| Aluminum alloys | Low density, corrosion resistance, machinability, and castability | Brackets, housings, engine and transmission components |
| Polypropylene | Low density, chemical resistance, and good processability | Trim, ducts, covers, and molded interior parts |
| Polyamide | Good strength, wear resistance, and temperature capability; moisture affects dimensions | Clips, brackets, connectors, and under-hood parts |
| ABS | Impact resistance, dimensional stability, and attractive molded surfaces | Interior trim, bezels, housings, and instrument-panel parts |
Finishes and protection used on harness builds
- Terminal plating: tin, silver or gold per the terminal specification.
- Bundle protection: PVC tape, cloth tape, conduit, braided sleeving or heat-shrink boots.
- Sealing: grommets, cavity seals and sealed connectors for splash or under-hood zones.
- Strain relief: overmolding, boots or clips where the drawing calls out a bend or pull requirement.
- Marking: labels, tags or print for circuit identification and traceability.
Wire harness assembly specifications and tolerances
Wire harness assembly specifications are set by the drawing, the process and the customer's requirements. The table lists the parameters to define before a harness is quoted and built.
| Parameter | Typical range | Standard or source |
|---|---|---|
| Dimensional tolerance | Unverified; depends on process, size, material, and drawing | Part drawing and supplier capability study required |
| Geometric tolerancing | Unverified; specify datum scheme and GD&T callouts | ASME Y14.5 or applicable ISO GPS standard; exact edition unverified |
| Surface roughness | Unverified; specify Ra or other required parameter | Drawing requirement; applicable surface-texture standard unverified |
| Hardness and strength | Unverified; defined by material and heat-treatment specification | Material specification and test method required |
| Capability | Cp/Cpk targets are customer- and feature-specific | IATF 16949, control plan, SPC, and customer-specific requirements |
| Part approval | Submission level and evidence vary by customer | AIAG PPAP and applicable customer-specific requirements |
Design tips that lower wire harness assembly cost
Most harness cost is fixed by the drawing, not by the build. These design choices reduce tooling, handling and test time without weakening the part.
- Standardize connector families and terminal part numbers across the harness so crimp tooling and applicators are shared.
- Request the tightest tolerance needed for function, not the tightest possible tolerance; the supplier should confirm capability for each critical feature.
- Keep branch lengths and breakouts on a clean grid so cut lengths and fixtures stay simple.
- Avoid unnecessary splices and welds; each joint adds validation, distortion risk and traceability work.
- Use one wire gauge per circuit where the current allows, rather than mixing gauges that complicate stripping and crimping.
- Place labels and clips where they can be applied after bundling, not inside a sealed or overmolded section.
- Define the test plan with the drawing: continuity only, or continuity plus pull and dimensional checks.
Typical automotive wire harness applications
Automotive wire harness work covers body, powertrain, chassis and interior circuits. The examples below show the range of cable harness assembly that can be quoted from a drawing.
- Engine and powertrain harnesses with sealed connectors and high-temperature cable.
- Body and door harnesses with grommets, boots and branch routing through hinge zones.
- Instrument-panel and console harnesses with molded connectors and tight bend radii.
- Battery and high-voltage cable assemblies with strain relief and shielding where specified.
- Sensor and actuator pigtails with overmolded joints and pull-tested crimps.
- Lighting, trailer and accessory harnesses for aftermarket and service programs.
- Test-fleet and prototype harnesses built before production tooling is committed.
Industries served include passenger vehicle, commercial vehicle, off-highway and specialty vehicle programs, plus aftermarket and performance parts where low-volume economics matter.
What drives wire harness assembly cost
No reliable universal price exists for a harness. Cost is built from the drawing, the components and the evidence the program requires, so two harnesses with the same branch count can price very differently.
- Cable type, gauge and length: total cut length and shielding or high-temperature cable raise material cost.
- Connector and terminal families: sealed, high-cavity or specialty connectors cost more than standard unsealed parts.
- Crimp and seal count: every termination adds labor, tooling and inspection time.
- Splices, welds and overmolding: each joint adds process steps and validation.
- Test and inspection level: continuity only versus continuity plus pull, dimensional and traceability records.
- Tooling and fixtures: applicators, test boards and build fixtures are amortized over the order quantity.
- Quantity and repeatability: higher volumes spread setup and tooling; prototypes carry more setup per unit.
- Logistics and packing: branch protection, reel or rack packing and delivery location affect cost.
Why order wire harness assembly through SR
Ordering wire harness assembly through SR gives you one contact for the program while a vetted network of automotive component manufacturers builds the parts. SR is a manufacturing broker and does not own factories or machines. It collects quotes, manages quality and inspection, and delivers the parts.
What SR does
- Collects quotes from a vetted supplier network against your drawing and quantity.
- Manages quality and inspection, including test records and dimensional checks.
- Delivers the finished harness to your delivery location.
- Keeps one point of contact for the program.
What you provide
- Harness drawing, wire list, connector schedule and revision.
- Material, finish, tolerance and inspection requirements.
- Quantity, delivery location and intended application.
- Any customer-specific requirements the program must meet.
Standards such as IATF 16949, APQP, FMEA, SPC and PPAP are applied as supplier and program requirements where the drawing or customer calls for them.
Have a drawing to quote?
Upload it with quantity and material to start a quote.
FAQ
Common questions
How much do custom auto parts cost?
No reliable universal price exists. Cost depends on geometry, material, process, tooling, quantity, tolerance, finishing, inspection, and logistics. For a harness, cable length, connector families, crimp count and test level drive most of the price.
What information is needed for a quote?
Provide CAD, drawing, revision, material, finish, tolerances, quantity, delivery location, inspection needs, and intended application. For a harness, add the wire list, connector schedule, branch lengths and any test plan.
What is PPAP?
PPAP is an automotive submission process used to demonstrate that production processes can consistently meet approved requirements; exact customer submission rules vary. It applies to harness builds when the program or customer requires it.
Can a supplier make a part without a drawing?
A supplier may reverse-engineer or develop a model, but requirements, ownership, tolerances, materials, and approval responsibilities must be agreed in writing. For harnesses, a documented wire list and connector schedule are needed before cutting starts.
Related resources
Keep reading


Ready when you are
Send your harness drawing for a quote
Share the drawing, wire list, connector schedule, quantity and delivery location. SR collects quotes from vetted suppliers and returns them in 5-7 working days.
Your files stay confidential. NDA available on request.