
Automotive Sourcing Service
Automotive Extrusions and Aluminum Parts Sourcing
Sourcing Repository collects quotes for automotive extrusions and other custom auto parts from a vetted supplier network, manages quality and inspection, and delivers parts to your dock.
- Aluminum for automotive
- Extruded profiles and assemblies
- IATF 16949 supplier requirements
- Quote in 5-7 working days
- One contact, one quoteSend CAD and drawing once; we manage suppliers.
- Inspection managedIncoming material and dimensional checks coordinated.
- PPAP supportSubmission evidence coordinated per customer requirements.
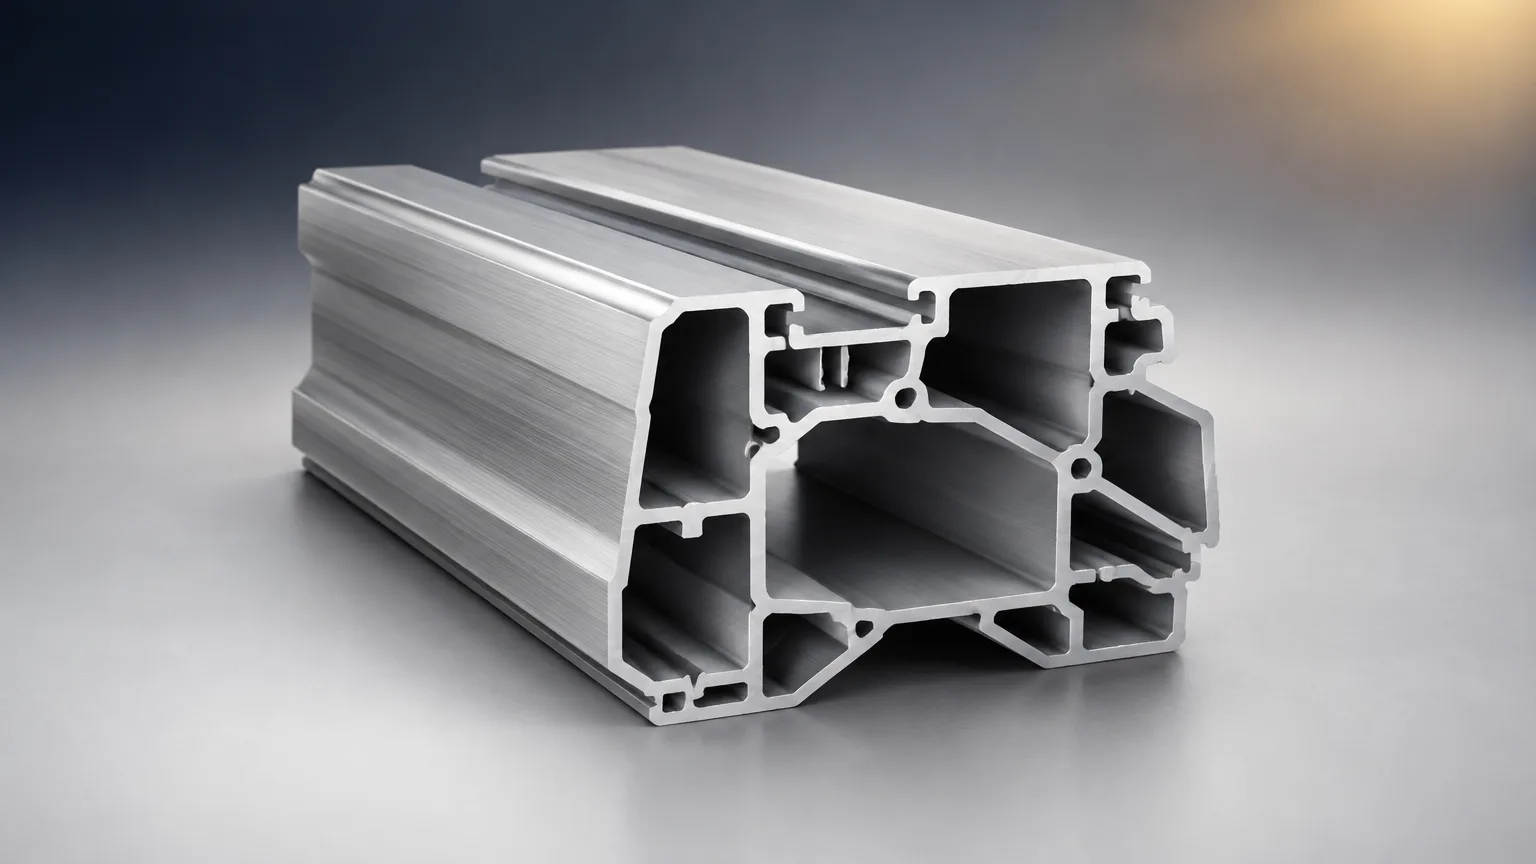
Automotive extrusions are aluminum profiles pressed through a die for structural, trim, thermal and crash-management parts in vehicles. Sourcing Repository is a manufacturing broker: it collects quotes from a vetted supplier network, manages quality and inspection, and delivers finished parts. Buyers send a drawing, material, finish and quantity; quotes typically return in 5-7 working days.
What automotive extrusions sourcing is and when to use it
Automotive extrusions are metal profiles formed by pushing heated billet through a shaped die, then cutting, machining, bending, joining and finishing them into vehicle components. They are a core process in auto parts manufacturing for parts with a constant cross-section.
Aluminum is the most common material because of its low density, corrosion resistance and formability, which is why buyers search for aluminum for automotive when they need lightweight structural or trim parts. This service suits engineers, procurement managers and founders sourcing custom profiles, machined extrusions or assemblies for automotive parts manufacturing, from prototype to production.
When to use an extrusion route
- The part has a constant cross-section, such as rails, sills, roof rails, battery-tray frames or heat-sink profiles.
- Weight reduction matters and aluminum can replace steel with a redesigned profile.
- You need low-to-medium volume custom auto parts without committing to high-volume stamping dies.
- Your customer, whether an OEM or a Tier 1 supplier, requires IATF 16949 and customer-specific requirements.
Automotive extrusion process steps
The automotive extrusion process runs in six steps, from requirements review to delivered parts. Each step produces a document or approval that the next depends on, so missing information early usually adds lead time later.
- 1. Requirements review You provide CAD, a drawing with revision, material, finish, tolerances, quantity and delivery location. We confirm the route, secondary operations and inspection needs.
- 2. Quote collection Sourcing Repository sends the package to vetted suppliers and returns a consolidated quote, typically within 5-7 working days.
- 3. DFM and tooling The selected supplier reviews die design, wall thickness, corner radii and alloy choice. Tooling is built and first-article parts are measured against the drawing.
- 4. Extrusion and secondary operations Billet is heated, pressed through the die and cut to length. Secondary operations may include CNC machining, bending, welding, anodizing, painting or assembly.
- 5. Inspection and documentation Incoming material verification, in-process checks and final inspection are coordinated. PPAP evidence is prepared where the customer requires it.
- 6. Delivery Parts are packed to protect the finish and shipped to the agreed location with traceability records and inspection reports.
Materials and finishes for automotive extrusions
Aluminum alloys are the main material for automotive extrusions, but the network also covers steel, magnesium, zinc and plastic routes when the part calls for them. Grade is unverified here and must be specified on the drawing.
| Material | Properties | Typical uses |
|---|---|---|
| Aluminum alloys | Low density, corrosion resistance, machinability, and castability | Brackets, housings, wheels, engine and transmission components |
| Carbon and alloy steel | High strength, fatigue resistance, hardness, and weldability vary by grade | Stampings, shafts, gears, suspension, fasteners, and structural parts |
| Magnesium alloys | Very low density and good castability; corrosion protection is often required | Lightweight housings, brackets, seat frames, and instrument-panel structures |
| Zinc alloys | Good die-castability, dimensional repeatability, and surface finish | Handles, latches, housings, and small hardware |
Finishes and surface treatments
- Anodizing for corrosion resistance and a controlled cosmetic surface on aluminum profiles.
- Powder coating or painting for color, UV resistance and chip protection.
- Conversion coating before bonding or painting.
- Welding, riveting, fastening or bonding for assemblies.
Automotive extrusion specifications and tolerances
Tolerances, size limits and lead times depend on the process, profile geometry, alloy and drawing. The table below lists the specification parameters the network works to; exact values are confirmed per part by the supplier capability study.
| Parameter | Typical range | Standard or source |
|---|---|---|
| Dimensional tolerance | Unverified; depends on process, size, material, and drawing | Part drawing and supplier capability study required |
| Geometric tolerancing | Unverified; specify datum scheme and GD&T callouts | ASME Y14.5 or applicable ISO GPS standard; exact edition unverified |
| Surface roughness | Unverified; specify Ra or other required parameter | Drawing requirement; applicable surface-texture standard unverified |
| Hardness and strength | Unverified; defined by material and heat-treatment specification | Material specification and test method required |
| Capability | Cp/Cpk targets are customer- and feature-specific | IATF 16949, control plan, SPC, and customer-specific requirements |
| Part approval | Submission level and evidence vary by customer | AIAG PPAP and applicable customer-specific requirements |
Design tips that lower automotive extrusion cost
Most extrusion cost is fixed at the design stage. These DFM rules reduce tooling, scrap and secondary operations without weakening the part.
- Keep wall thickness uniform along the profile; abrupt changes cause distortion and slow the press.
- Use generous corner radii and avoid sharp internal corners that wear the die.
- Design for the tightest tolerance that function requires, not the tightest the process can hold.
- Minimize secondary machining by placing features where the die can form them.
- Standardize on one or two alloys across a family of parts to simplify material buying.
- Add a datum scheme and GD&T callouts on the drawing so inspection is unambiguous.
- Plan the finish early; anodizing and coating add handling and masking steps.
Typical automotive extrusion applications
Typical automotive extrusion applications span body, chassis, powertrain, thermal and interior systems in car parts manufacturing and vehicle parts manufacturing. The examples below show where the network is commonly asked to quote.
- Structural rails, sills, bumper beams and crash-management profiles.
- Battery-tray frames, module housings and thermal-management channels for electric vehicles.
- Roof rails, window frames and door trim.
- Heat sinks, heat exchangers and cooling plates.
- Seat frames, instrument-panel structures and under-hood brackets.
OEM production programs
- Validated processes and traceability
- IATF 16949 and customer-specific requirements
- PPAP submission and control plans
Custom and aftermarket work
- Flexibility and low-volume economics
- Prototype and bridge production
- Reverse engineering possible with written agreement
What drives the cost of automotive extrusions
The cost of automotive extrusions is built from material, tooling, processing, finishing, inspection and logistics, and it changes with quantity and tolerance. No reliable universal price exists for custom auto parts.
- Material type, grade, availability and buy-to-fly ratio.
- Part geometry, size, wall thickness and tolerance requirements.
- Die and tooling cost, amortized over the order quantity.
- Secondary operations such as machining, bending, welding and assembly.
- Finish type, inspection level and PPAP evidence.
- Order quantity, packaging and delivery location.
Prototype routes minimize tooling and lead time; production routes optimize repeatability, cycle time, capability and total cost.
Why order automotive extrusions through Sourcing Repository
Ordering automotive extrusions through Sourcing Repository gives buyers one contact instead of a supplier list. Sourcing Repository is a manufacturing broker; it does not own factories or machines, but collects quotes from a vetted supplier network, manages quality and inspection, and delivers parts.
- Vetted network: automotive component manufacturers are screened for capability, process control and automotive experience.
- One contact: send the RFQ once and receive a consolidated quote, typically in 5-7 working days.
- Quality management: incoming material verification, in-process checks and final inspection are coordinated.
- Documentation: PPAP evidence and control-plan records are prepared where the customer requires them.
- Delivery: parts are packed and shipped to the agreed location with traceability records.
Have a drawing to quote?
Upload it with quantity and material to start a quote.
FAQ
Common questions
How much do custom auto parts cost?
No reliable universal price exists. Cost depends on geometry, material, process, tooling, quantity, tolerance, finishing, inspection and logistics. Send a complete drawing and quantity so suppliers can quote the actual part rather than a range.
What information is needed for a quote?
Provide CAD, drawing and revision, material, finish, tolerances, quantity, delivery location, inspection needs and the intended application. Missing any of these usually delays the quote because suppliers must confirm feasibility before pricing.
What is PPAP?
PPAP is an automotive submission process used to demonstrate that production processes can consistently meet approved requirements. Exact submission levels and evidence vary by customer, so confirm the required level before production starts.
Can a supplier make a part without a drawing?
A supplier may reverse-engineer or develop a model, but requirements, ownership, tolerances, materials and approval responsibilities must be agreed in writing. A drawing or approved 3D model is still needed before production.
Related resources
Keep reading


Ready when you are
Get a quote for automotive extrusions
Send your drawing, material, finish and quantity. Sourcing Repository collects quotes from a vetted supplier network and returns a consolidated quote, typically in 5-7 working days.
Your files stay confidential. NDA available on request.